
TIG welding aluminum settings can be overwhelming if you haven’t welded this material before. The charts below should help you get started, while our full guide on TIG welding aluminum can clear any process doubts.
The charts below show a good starting point for welders TIG welding aluminum for the first time. However, your power source, travel speed, technique, tungsten stickout, TIG cup size, and the joint type will all affect the actual amperage and other values. Use them as a guide rather than a hard rule.
TIG Welding Aluminum Amperage Chart
Amperage controls heat input, which determines whether you achieve full penetration or burn through the base material. Aluminum conducts heat about 4-5X faster than carbon steel, and about 10-12X faster than stainless steel. So, compared with steel of the same thickness, aluminum generally requires more amperage. However, with a low melting point, thin sheet aluminum will burn through with excessive amperage.
A common starting rule of thumb is 1 amp per 0.001 inches of material thickness, though aluminum’s thermal conductivity can sometimes push that number higher in practice. Some welders like to use 1.2 amps per 0.001 inches as a rule of thumb for aluminum, but this depends on personal experience. Above 1/4″, joint preparation, preheat, and multiple passes can matter more than simply increasing amperage.
The table below gives starting points for AC aluminum TIG welding across common thicknesses, but you might need to do some trial and error to match your preferred speed.
You can also download our recommended starting range TIG welding aluminum settings in a free PDF.
Material Thickness | Amperage Range* | Filler Rod Diameter | Tungsten Electrode Diameter |
1/16″ (1.6 mm) | 55–80 | 1/16″ (1.6 mm) | 1/16″ (1.6 mm) |
1/8″ (3.2 mm) | 110–160 | 3/32″ (2.4 mm) | 3/32″ (2.4 mm) |
3/16″ (4.8 mm) | 130–215 | 3/32″ (2.4 mm) | 3/32″–1/8″ (2.4 mm–3.2 mm) |
1/4″ (6.4 mm) | 150–260 | 3/32″–1/8″ (2.4 mm–3.2 mm) | 1/8″–5/32″ (3.2–4.0 mm) |
3/8″ (9.5 mm) | 290–380 | 3/16″ (4.8 mm) | 5/32″–3/16″ (4.0–4.8 mm) |
* Amperage values depend on weld type, joint design, fit-up, travel speed, preheat, foot pedal use, and whether full penetration is required. Outside corner welds often need less current, while lap, T-joint, butt, and fillet welds may require more.
TIG Welding Aluminum Gas Flow Settings
Aluminum is highly reactive when molten. Oxygen and nitrogen contamination happen quickly without adequate argon shielding. The result is a dull, porous weld with poor fusion. Pure argon is the standard shielding gas for AC TIG welding aluminum. While helium blends can increase penetration on thicker sections, argon is the best choice for most applications.
Gas flow rate is set by cup size, not material thickness. The goal is steady, laminar coverage over the weld pool.
- Insufficient flow leaves the puddle exposed to the air.
- Excessive flow creates turbulence that draws in atmospheric air from the edges.
A useful starting rule is to multiply the cup number by 2–3 CFH (cubic feet per hour). Gas lens setups improve shielding consistency and allow slightly lower flow rates for equivalent protection — worth using on aluminum whenever practical.
TIG Cup Size | Nozzle Inside Diameter | Gas Flow (CFH) |
#4 | 1/4″ (6.4 mm) | 10–14 |
#5 | 5/16″ (8.0 mm) | 11–15 |
#6 | 3/8″ (9.5 mm) | 12–16 |
#7 | 7/16″ (11.1 mm) | 13–18 |
#8 | 1/2″ (12.7 mm) | 17–23 |
#10 | 5/8″ (15.9 mm) | 20–31 |
#12 | 3/4″ (19.0 mm) | 25–40 |
You should always try to use the least gas flow you need. More isn’t better. Use more only if the lower value is insufficient for the environment, joint, and setup conditions.
Factors that affect the shielding gas flow requirements are:
- Tungsten stickout: 1/4″–3/8″ usually requires standard flow, while above 3/8″ needs higher flow.
- Welding position: flat uses standard flow rates. Vertical up and overhead require fine-tuning with higher flow.
- Drafts: If there’s no draft, use standard flow. Increase the flow to compensate for the draft. You may need 20-50% higher flow.
TIG AC Frequency And Balance Settings Chart
AC welding alternates between two halves of the cycle:
- Electrode negative (EN) drives heat into the base material for penetration.
- Electrode positive (EP) blasts apart the tough aluminum oxide layer on the part surface. Otherwise known as the cleaning action.
AC balance controls the ratio between them.
A higher EN percentage (around 70–75%) means more penetration and less cleaning. A lower EN percentage (around 50–65%) means a wider cleaning zone, useful on dirty or oxidized material. The more you pre-clean the aluminum, the more EN you can run.
Condition | AC Balance | Cleaning Action |
Perfectly clean material, max penetration | 15% EP, 85% EN | Low |
Standard clean aluminum (This is the best starting point) | 25-30% EP, 70-75% EN | Moderate |
Lightly oxidized | 35% EP, 65% EN | High |
Oxidized, cast aluminum | 50%EP, 50% EN | Highest |
The AC balance effect will vary across welding machines. 70EN/30EP is the best starting point for high quality aluminum welds, especially for beginners. Experiment with lower and higher settings to fine-tune for your machine and the job.
You can use up to 50% EP if the part requires it, but the arc may be more erratic, and you’ll get a very wide cleaning pool with reduced penetration. You might need a size larger tungsten than usual if you have to use a 40-50% EP portion of AC because it may melt or excessively ball up your tungsten.
AC Frequency controls how many times per second EN and EP switch in AC (Hertz, Hz).
A high frequency creates a focused arc with deeper heat input. It’s better for precise work, fillets, and directional control on thinner material.
A low frequency produces a soft, wide arc with shallow heat input. It works well for filling wider joints and build-up.
Application | AC Frequency |
Wide beads, build-up, thicker plate | 40–80 Hz |
General-purpose welding | 100–120 Hz |
Thin material, tight fillets, precision work | 150–250 Hz |
Pulse TIG Welding Aluminum Settings
Pulsed TIG rapidly alternates between a high peak current and a low background current. The peak does the melting; the background lets the puddle cool slightly before the next pulse. Pulsed TIG reduces the heat input, which is critical to prevent distortion and burn-through on thin material.
There are four settings to dial in:
- Peak amperage — your main welding current. Set it using the amperage chart.
- Background amperage — expressed as a percentage of peak, typically 10–50%. This is your puddle’s “rest” current. On Fronius welders, this is set as “Base current,” where you set the percentage of your main current. So, with Fronius, you just set this percentage, and you get both peak and background set simultaneously.
- Pulse frequency (pulses per second) — how fast it switches. Low frequency (0.5–5 Hz) is visible pulsing for manual filler metal timing; high frequency (100+ Hz) stiffens and focuses the arc, increases arc stability, and boosts travel speed. Fronius allows up to 2000 Hz (10,000 Hz with OPT/I-Pulse Pro option), which can be beneficial for arc focusing in automated welding applications.
- Pulse duty cycle (peak time %) — the percentage of each pulse spent at peak current, usually 30–50%. This has a high effect on heat input.
AC Offset Settings: Independent Amperage Control For AC
AC offset shifts the overall current balance toward the positive or negative, letting you tune heat distribution beyond what standard EN/EP balance allows. It lets you control the actual amperage for EN and EP cycles of AC. On Fronius power sources, it’s adjustable from −70% to +70%. Most TIG welders don’t support this feature, but it can be valuable.
The effect is straightforward:
AC Offset | Arc Behavior |
+70% | Wide arc, shallow heat input |
0% (factory) | Balanced starting point |
−70% | Narrow arc, deep heat input, higher welding speed |
Push positive for thin sheet and wide beads; push negative for thicker material, deeper penetration, and faster travel.
Robotic TIG Welding Is Consistently Reliable
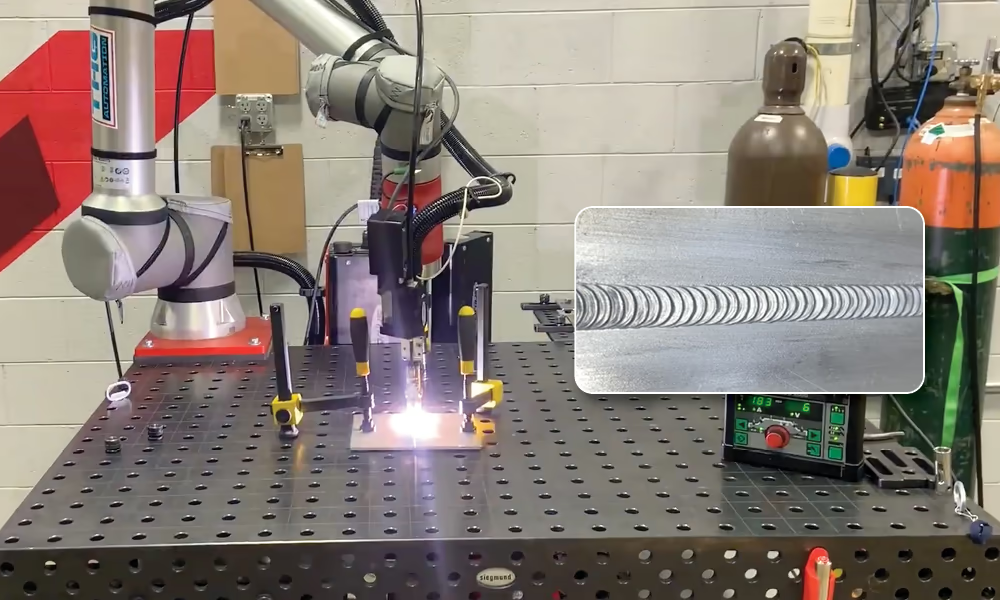
Everything discussed so far comes down to one challenge: applying the right settings and welding technique consistently, weld after weld. TIG welding settings only matter if you can reproduce them. And by hand, even skilled welders can drift over a long run.
With manufacturers and small shops struggling with a labor shortage, welders are overwhelmed. This makes it even more likely for human error to creep in and increase scrap and rework.
This is where collaborative robot welding has become practical for smaller shops. Once the realm of large production lines and six-figure budgets, robotic welding is now accessible to job shops and fabricators running high-mix, low-volume work.
A cobot doesn’t replace welding knowledge. The settings in this guide still have to be correct. What it does is execute them identically every time, removing the run-to-run variation that causes inconsistent penetration, uneven beads, and rework.
And you don’t need specialized robotic welding or programming skills.
However, automation isn’t a magic fix. A cobot welds exactly what it’s programmed to weld, so a flawed process just produces flawed parts faster. The value comes from pairing a properly dialed-in process with a system that repeats it precisely.
THG Automation modular cobot welding systems are designed to grow with a shop’s production rather than lock it into a fixed setup, with welding engineers and CWIs who help get the process right before deployment. We don’t just hand over a start button and disappear.
THG’s TIG welding robotic systems support floor and table positioners, coordinated motion, tracks, manual and robot welding modes, automated process switching, and more. No experience required.
If you’re weighing whether automation makes sense for your aluminum work, talk to our fabrication experts. Or, learn more in our case studies where we routinely improve welding throughput by 2-7X for our customers.